Explore our cutting-edge machinery designed for high-efficiency liquid concentration, advanced separation, and thermal management.
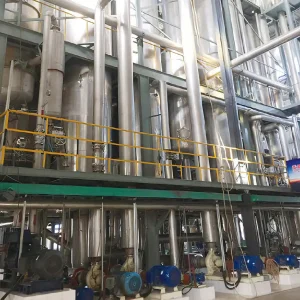
Top China Suppliers and Factory for Efficient Liquid Concentration Solutions Manufacturers, Factory
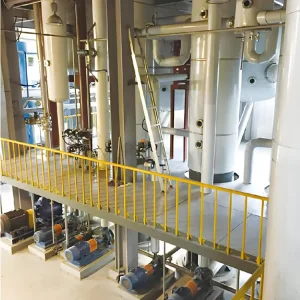
China Suppliers and Factory for Heat-Sensitive Liquid Concentration Manufacturers, Service
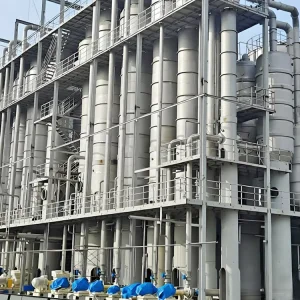
China Suppliers Factory Waste Heat Evaporator for Efficient Wastewater Treatment and Reduced Steam Consumption
High-Quality Factory Solutions for Heat-Sensitive Liquids Supplier, Service from China Suppliers
Leading China Suppliers & Factory Solutions Supplier, Service for industrial fluid concentration
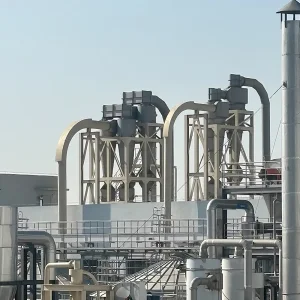
Jiangsu Zongheng Factory Manufacturers, Service delivering rapid and uniform material drying
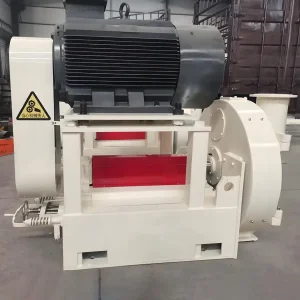
High Precision Corn Processing Factory Solutions engineered for maximum germ recovery
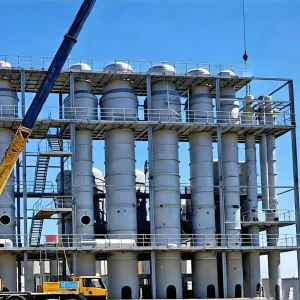
Zongheng Industrial Factory Manufacturer, Supplier providing state-of-the-art thermal engineering
Bridging heavy thermal engineering with strict CE compliance and high-performance equipment procurement standards worldwide.
In modern industrial manufacturing—ranging from chemical processing plants and petrochemical refineries to large-scale bio-fermentation and starch processing facilities—efficient thermal energy management is the core determinant of operational profitability. Global enterprise procurement teams continuously search for verified CE Certification Cooling Tower Suppliers & Factory partners who guarantee stringent safety compliance, lower carbon footprints, and uninterrupted duty-cycle reliability.
Jiangsu Zongheng Concentrating and Drying Equipment Co., Ltd. answers this global demand by incorporating advanced thermodynamic modeling into every evaporation, drying, and cooling solution. By unifying mechanical durability with high-precision fabrication, our systems integrate seamlessly into international plant architectures.
A strategic overview of how next-generation thermal engineering and digital monitoring are transforming global manufacturing.
Integrating waste heat recovery evaporators with closed-loop cooling towers to harness secondary thermal output, drastically cutting overall steam consumption across chemical and food-processing lines.
Deploying real-time telemetry, predictive maintenance algorithms, and automated fluid dynamics balancing to secure maximum uptime and proactive fault prevention across international facilities.
Achieving zero-discharge environmental standards through elite mechanical vapor recompression (MVR) and starch cyclone washing systems aligned with stringent global ecological directives.
Discover our comprehensive inventory of heavy-duty presses, dryers, and separation technologies built to global certification standards.
Reliable Suppliers from a Leading Factory for Efficient Dewatering in industrial applications
China Suppliers Factory Waste Heat Evaporator for Corn Steep Liquor and Wastewater Treatment Solutions
China Suppliers Factory: Efficient Dewatering of Corn Fiber and Germ with high solid recovery
Leading Suppliers & Factory for Precision Germ Removal in Maize Processing lines
Efficient High-Speed Hot Air Technology for Uniform Material Drying across multiple sectors
Efficient Drying Solution from Jiangsu Zongheng Factory engineered for continuous throughput
High-Efficiency, Cost-Saving Solutions from Leading Suppliers with low operational expenditure
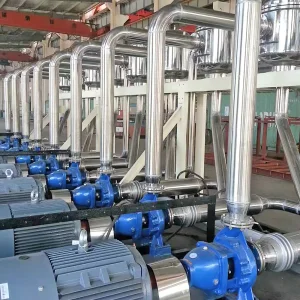
China Suppliers Factory: Effective Starch Refining and Purity Enhancement for food industry
Insights into global standards, international certifications, and technical support frameworks.
Our manufacturing plant operates under rigorous international standards, holding ISO9001 quality system certification, ASME "U" Stamp authorization, and special equipment manufacturing licenses, ensuring complete compliance for European and global markets.
We provide comprehensive engineering documentation, remote telemetry commissioning, and dedicated on-site installation guidance backed by our team of 20+ senior mechanical engineers, ensuring smooth integration anywhere in the world.
By leveraging advanced Mechanical Vapor Recompression (MVR) and optimized waste heat recovery architectures, our systems recycle secondary thermal energy, reducing primary steam and electrical consumption by up to 50%.
With over 30 years of manufacturing excellence, a 54,000+ square meter state-of-the-art facility, and thousands of successful global deployments in chemical, food, and pharmaceutical sectors, we deliver unmatched reliability and engineering integrity.
 Zongheng